Fermentieren
9. May 2025Read more

28. August 2026
Wherever food is produced, even minor mix-ups can have far-reaching consequences. If, for example, a scoop from a production area containing allergens ends up on another production line, there is a risk of cross-contamination, which can have far-reaching consequences. Colour-coding work equipment is a straightforward way to quickly ensure clarity and unambiguous allocation. Different colours indicate which process or area a piece of equipment belongs to, or what it is intended for. Colour coding is a useful addition to cleaning schedules, HACCP schemes and other hygiene measures. For this reason, we are taking a closer look at what colour coding is all about.
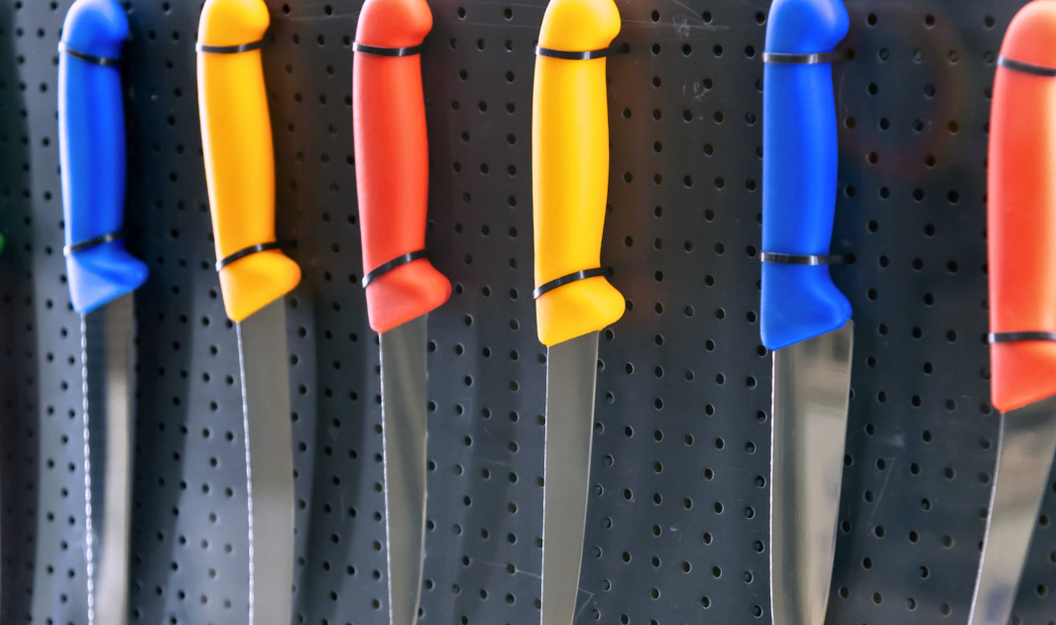
As part of the colour-coding system, specific colours are assigned to relevant areas within a food production facility. The equipment used within this area is given a corresponding colour code. The classification may vary, for example by production zone, product group, allergen, cleaning stage or risk level. A useful distinction may also be made between equipment for raw and ready-to-eat food.
It is important that a colour scheme is clear and consistently applied. The colour code should appear on work equipment, at the storage location, in the cleaning schedule and in the relevant operating instructions. This enables staff to see at a glance where an item or tool is used and stored. This makes it easier to keep work equipment separate and reduces the risk of Cross-contamination – Of course, this is no substitute for professional cleaning and a workplace risk assessment.
Although the colour scheme should ideally be recognisable throughout the entire area, it is easiest to implement with manual cleaning equipment and smaller items of workwear. However, components of disposable clothing are also available in different colour schemes. Examples of workwear items that are frequently colour-coded include:
Hand brushes, tank brushes and pipe brushes
Brooms, scrubbing brushes and squeegees
BUCKETS, tubs and dustpans
Scrapers, spatulas and dough cutters
Hand, product and Measuring scoops
Chopping boards, knives and tongs
Containers, lids and waste bins
Cleaning wipes, protective gloves and other cleaning aids
Disposable clothing such as aprons, hoods / hair nets or gloves
Colour-coding is most easily recognisable when equipment is entirely in the relevant colour or features permanently integrated, hygienically suitable coloured elements. This is usually more reliable than adhesive tape or labels, which can come loose or become illegible. Specific holders or so-called ‘shadow walls’ ensure that each piece of equipment has a fixed place, making it immediately apparent if something is missing or has been placed incorrectly.
The greatest advantage of colour-coding is that it can be grasped at a glance. This, in turn, has a positive impact on other factors, which is why, for example, the consistent use of colour-coding brings the following benefits:
reduced risk of the transmission of microorganisms, allergens and foreign bodies
Reduced search times thanks to well-organised workspaces
greater traceability during inspections and audits
easier induction and training of new staff thanks to clear responsibilities
Early detection of work equipment that has been misplaced
longer service life thanks to appropriate storage in the relevant work area
When implemented correctly, colour-coding therefore not only supports food safety but also improves operational efficiency. Equipment is found more quickly, returned to its proper place and is less likely to end up in the wrong areas.
There is no universally applicable colour scheme for work equipment and work areas. Organisations can develop their own colour schemes that are suited to their products, processes and the associated risks. Blue, red, green, yellow and white are widely used, sometimes supplemented by other colours such as orange, pink or purple – for example, in particularly high-risk areas. It is advisable to use as few colours as possible, as too many colour schemes unnecessarily complicate the system and increase the risk of confusion.
It is also a good idea to choose colours that contrast with the colours of the foodstuffs that are mainly processed there. This makes it easier to spot foreign objects such as broken bristles or plastic parts.
Furthermore, it is important that colour coding is not the only criterion used for classification. Supplementary symbols, numbers or labels are not only of benefit to people with colour vision deficiency.
Within food production facilities, staff encounter a variety of colours for hygiene purposes, even beyond the colour-coding system. The colours chosen on an individual basis must not interfere with the requirements for health and safety signage in workplaces as specified in ASR A1.3. In safety signage, colours such as red, yellow, green and blue have clearly defined meanings. They indicate, for example, prohibitions, warnings, instructions, escape routes, first-aid facilities or fire safety equipment. The company’s colour-coding system must not impair the visibility or clarity of these safety signs.
The German Social Accident Insurance (DGUV) also recommends a standardised colour scheme for operating instructions. Accordingly, blue operating instructions are intended for machinery, green for personal protective equipment and orange or red for hazardous substances. This colour scheme therefore serves a different purpose to hygiene colour codes and should be clearly distinguishable from them.
There is no general statutory requirement mandating the use of colour coding in the food industry. However, food businesses must, as a matter of principle, establish, implement and maintain procedures that are based on the HACCP-principles. In doing so, relevant hazards must be identified and, through appropriate measures, prevented, eliminated or reduced to an acceptable level.
In addition to the results of the risk assessment, certification standards may also require the clear classification and labelling of cleaning and disinfection equipment. Labelling using a colour-coding system is a suitable method in this context, but it is not the only one.
The decision to introduce colour-coding should always be based on an operational risk assessment. This involves, for example, identifying where raw and ready-to-eat food come into contact, or where Allergens be processed. Colours can then be assigned and the necessary equipment identified.
Once a system has been defined, it should also be documented in cleaning schedules, operating instructions and training materials. Signs featuring text, colours and symbols support its day-to-day use. All staff, including external cleaning staff, must be familiar with the system.
As in every aspect of responsible food production, checks are essential here too. The colour-coding system and the correct allocation of equipment should be checked regularly. Any equipment that is damaged, worn out or no longer clearly identifiable must then be replaced.
When procuring colour-coded work equipment, a centralised and standardised purchasing process is particularly advantageous. This ensures that colours, materials and designs are consistently compatible. Furthermore, it is advantageous to be able to reliably source all the necessary supplies and consumables for food production from a single supplier.
With our wide range of products, we have been supplying food production businesses with high-quality items for over a century. From spices to tools and work equipment, right through to technical apparatus, you will find a wide range of solutions for safe, hygienic and efficient production processes.


More articles